5052 H48 Can End Aluminum Coil
145 Views 2026-09-21 08:46:23
1. Introduction
5052 H48 Can End Aluminum Coil is a 5xxx-series aluminum product used for selected can-end and closure applications.
It combines good corrosion resistance, controlled strength, lightweight construction, and suitable forming performance.
5052 is a non-heat-treatable aluminum-magnesium alloy. Its strength mainly comes from magnesium alloying and cold working, while the H48 temper provides a higher-strength condition for demanding processing applications.
For can-end production, consistent thickness, mechanical properties, flatness, surface quality, and edge condition are essential.
These factors affect blanking, forming, scoring, curling, riveting, and coating performance.
ASTM B209/B209M provides an important specification framework for aluminum sheet and coiled sheet.
However, the final material requirements should also match the specific can-end design, thickness, forming process, and performance requirements.
Compared with other can-end alloys such as 5182 H48, 5052 H48 offers a different balance of strength, corrosion resistance, and formability.
Therefore, alloy and temper selection should follow the requirements of the finished can end rather than alloy designation alone.

Custom 5052 H48 Can End Aluminum Coil
2. What Is 5052 H48 Can End Aluminum Coil?
5052 H48 Can End Aluminum Coil is a 5xxx-series aluminum-magnesium coil supplied in the H48 temper for selected can-end and closure applications.
It combines good corrosion resistance, increased strength, lightweight construction, and controlled forming performance.
2.1 5052 Aluminum Alloy
5052 aluminum coil is a non-heat-treatable aluminum alloy. Magnesium provides its main strengthening effect, while chromium helps control the microstructure.
The alloy gains additional strength through cold working rather than precipitation heat treatment.
2.2 H48 Temper
The H48 temper indicates a strain-hardened condition. Compared with softer 5052 tempers, H48 provides higher strength and hardness while maintaining useful forming characteristics.
For can-end production, consistent temper control helps maintain stable performance during blanking, forming, scoring, curling, and riveting.
2.3 Can End Aluminum Coil
Can-end aluminum coil is supplied in continuous coil form for high-speed blanking and forming operations.
Depending on the can design, the material may undergo:
- Blanking
- Shell forming
- Curling
- Countersinking
- Scoring
- Riveting
- Coating
Because the coil feeds continuously through production equipment, thickness consistency, flatness, surface quality, edge condition, and mechanical properties are critical.
2.4 Key Characteristics
5052 H48 can-end coil is mainly selected for its:
- Good corrosion resistance
- Higher strength in H48 temper
- Lightweight construction
- Controlled forming performance
- Good surface quality
- Compatibility with protective coatings
The material should be selected according to the specific can-end design, thickness, forming process, and performance requirements.
For higher-strength applications, manufacturers may also consider alternatives such as 5182 H48.

5052 H48 Can End Aluminum Coil
3. Chemical Composition of 5052 Aluminum
The chemical composition of 5052 provides the foundation for its mechanical properties, corrosion resistance, and processing behavior.
Magnesium is the principal alloying element, while chromium contributes to microstructural control.
Other elements remain within controlled limits to maintain the intended performance of the alloy.
Typical composition limits for 5052 aluminum are shown below.
Exact requirements should always be confirmed against the applicable material standard and purchase specification.
3.1 Typical Chemical Composition
| Element | Typical Composition, wt.% | Main Function |
|---|---|---|
| Magnesium (Mg) | 2.2–2.8 | Main strengthening element |
| Chromium (Cr) | 0.15–0.35 | Microstructure control and corrosion-related performance |
| Iron (Fe) | ≤ 0.40 | Controlled impurity |
| Silicon (Si) | ≤ 0.25 | Controlled impurity |
| Copper (Cu) | ≤ 0.10 | Controlled to maintain alloy characteristics |
| Manganese (Mn) | ≤ 0.10 | Microstructure control |
| Zinc (Zn) | ≤ 0.10 | Controlled impurity |
| Other Elements | ≤ 0.05 each / ≤ 0.15 total | Trace-element control |
| Aluminum (Al) | Balance | Base metal |
Exact chemical limits depend on the applicable standard or customer specification.
4. Specifications of 5052 H48 Can End Aluminum Coil
5052 H48 Can End Aluminum Coil should be specified according to the requirements of the finished can end and the production line.
Alloy, temper, thickness, width, surface condition, coil dimensions, and mechanical properties are the core specifications.
4.1 Core Specifications
| Parameter | Typical Specification |
|---|---|
| Alloy | 5052 |
| Temper | H48 |
| Product Form | Aluminum Coil |
| Main Application | Can Ends / Closure Components |
| Thickness | Customized according to can design |
| Width | Customized / Slit Width |
| Surface | Smooth, clean, uniform |
| Edge | Slit or mill edge, controlled burr |
| Coil ID/OD | According to production line requirements |
| Coil Weight | Customized |
| Standard | ASTM B209/B209M or applicable customer specification |
| Coating | Bare, lacquered, or coated according to application |
The exact dimensional range should be agreed between the aluminum supplier and can manufacturer because can-end geometry, tooling, and production equipment can impose specific requirements.
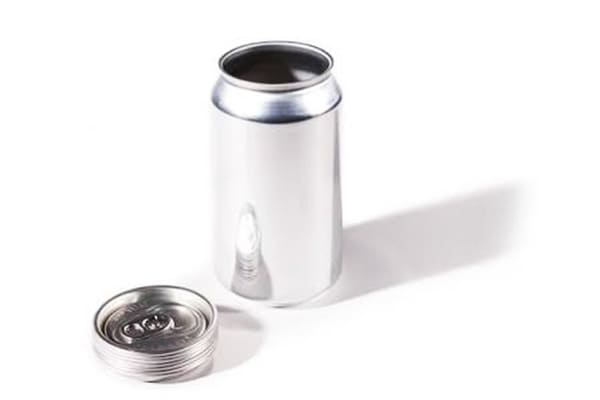
Can End and Can Body
5. Mechanical and Physical Properties
The mechanical properties of 5052 H48 depend on the applicable standard, product thickness, and processing condition.
Therefore, manufacturers should use the values specified for the actual product rather than relying on a single universal value.
5.1 Mechanical Properties
The key mechanical parameters include:
- Tensile strength
- Yield strength
- Elongation
- Hardness
H48 provides substantially higher strength than annealed 5052 because the material undergoes controlled cold working.
For can-end applications, strength should be sufficient to maintain the required shape while still allowing the material to undergo forming, scoring, and other conversion processes.
Mechanical Properties — Key Considerations
| Property | Importance for Can Ends |
|---|---|
| Tensile Strength | Supports structural strength and resistance to deformation |
| Yield Strength | Helps maintain dimensional stability during use |
| Elongation | Indicates available forming capability |
| Hardness | Influences forming, scoring, and tool interaction |
| Temper Uniformity | Supports consistent high-speed production |
Actual mechanical-property requirements should follow the applicable material standard and customer specification.
5.2 Physical Properties
5052 aluminum has the typical lightweight characteristics of wrought aluminum alloys.
| Physical Property | Typical Value |
|---|---|
| Density | Approx. 2.68 g/cm³ |
| Elastic Modulus | Approx. 70–72 GPa |
| Poisson’s Ratio | Approx. 0.33 |
| Melting Range | Approx. 607–649°C |
| Thermal Conductivity | Approx. 138 W/m·K |
These values are general reference data and may vary slightly with material condition and source.
5.3 Why These Properties Matter
For can-end manufacturing, the most important properties are not simply maximum strength or lowest density.
The material must provide a balanced property profile.
A suitable 5052 H48 coil should combine sufficient strength with controlled elongation, stable dimensions, good surface quality, and predictable forming behavior.
6. Key Performance Requirements for Can End Aluminum Coil
Can-end aluminum coil must meet both material requirements and conversion-process requirements.
A coil that meets the basic chemical composition but performs inconsistently during forming may still create production problems.
6.1 Strength and Dimensional Stability
The H48 temper provides increased strength through strain hardening. This helps the finished can end resist deformation during handling and service.
Consistent yield strength is also important because variations can change forming behavior from one coil to another.
For pressurized packaging, the final end design and material thickness must be evaluated together rather than relying on alloy strength alone.
6.2 Formability
Can-end production involves several forming operations. The material must deform in a controlled manner without excessive cracking or distortion.
Important forming operations include:
- Shell forming
- Countersinking
- Curling
- Scoring
- Rivet formation
- Tab attachment
Formability depends on the combination of alloy, temper, thickness, lubrication, tooling, and forming speed.
6.3 Scoring Performance
Scoring creates a controlled weakened line that allows the consumer to open the can.
The score must provide a carefully controlled balance:
Strong enough to resist premature opening + weak enough to open reliably
Material consistency is therefore critical. Variations in thickness, hardness, or mechanical properties can influence score depth and opening behavior.
6.4 Corrosion Resistance
Can ends may encounter moisture, atmospheric exposure, and contact with packaging contents.
5052 provides good corrosion resistance for many environments, but the finished packaging system often relies on an appropriate internal or external coating for additional protection.
Coating selection should consider:
- Product chemistry
- Storage conditions
- Processing temperature
- Food-contact requirements
- Coating adhesion
- Chemical resistance
6.5 Surface Quality
Surface quality directly affects both appearance and downstream coating performance.
The coil should maintain a clean, uniform surface with controlled levels of:
- Scratches
- Pits
- Dents
- Oil residue
- Oxidation
- Surface marks
Consistent surface quality is particularly important when the can end requires lacquer, printing, or other surface treatment.
6.6 Edge Quality
Coil edges must remain stable during feeding and blanking.
Excessive burrs, cracks, or damaged edges can cause:
- Feeding problems
- Tool wear
- Edge cracking
- Material waste
- Production interruptions
Controlled slitting and edge inspection therefore form an important part of can-end coil quality control.
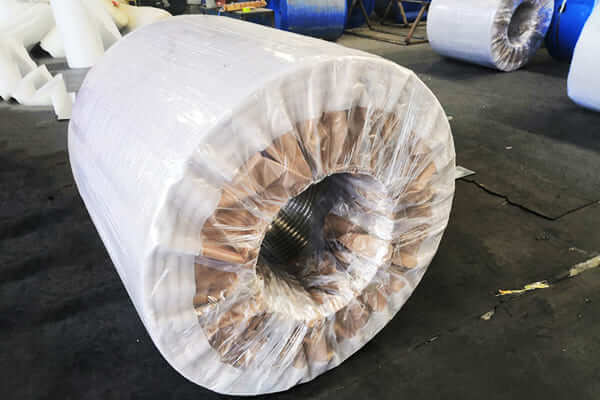
Huawei Packaged 5052 H48 Aluminum Coil
7. Manufacturing Process of 5052 H48 Can End Aluminum Coil
The production of 5052 H48 can-end coil combines metallurgical control, rolling technology, temper processing, surface finishing, and final inspection.
7.1 Alloy Melting and Casting
The process begins with carefully controlled aluminum alloy preparation.
The required levels of magnesium, chromium, and other elements are adjusted according to the applicable 5052 specification.
The molten aluminum then undergoes purification and casting.
Control at this stage helps minimize inclusions and maintain consistent chemical composition.
7.2 Homogenization
After casting, the aluminum may undergo homogenization treatment to reduce chemical segregation and improve microstructural uniformity.
A controlled microstructure provides a more stable foundation for subsequent hot rolling and cold rolling.
7.3 Hot Rolling
The cast material is processed through hot rolling to reduce its thickness and produce a suitable intermediate strip.
Hot rolling helps:
- Refine the material structure
- Reduce casting-related variations
- Improve internal consistency
- Prepare the material for cold rolling
Rolling parameters must remain tightly controlled to achieve the required thickness and surface quality.
7.4 Cold Rolling
Cold rolling provides precise thickness reduction and contributes directly to the strain-hardening response of 5052.
For H48 material, controlled cold working is particularly important because it determines much of the final strength and hardness.
During this stage, manufacturers monitor:
- Thickness
- Flatness
- Surface quality
- Rolling reduction
- Coil tension
- Edge condition
7.5 Temper Control
The material is processed to achieve the specified H48 temper.
Because the temper directly influences strength, hardness, and forming behavior, manufacturers must maintain consistent processing conditions across the coil.
Quality control normally includes mechanical testing to verify that the finished material meets the required specification.
7.6 Surface Treatment or Coating
Depending on the application, the coil may be supplied as bare aluminum or with a specified coating/lacquer system.
For coated can-end material, the process may include:
- Surface cleaning
- Pretreatment where required
- Primer or lacquer application
- Controlled curing
- Coating inspection
The coating must provide suitable adhesion and resistance for the intended packaging environment.
7.7 Slitting and Coil Finishing
Large-width aluminum coils can be slit into narrower widths according to the customer’s production requirements.
During slitting, manufacturers control:
- Width tolerance
- Edge burr
- Edge cracking
- Coil tension
- Winding quality
- Coil alignment
Proper slitting is essential for stable feeding into downstream can-end production equipment.
7.8 Packaging and Shipment
The final coils should receive suitable packaging to protect them from moisture, impact, contamination, and edge damage during transportation.
For export orders, packaging should be adapted to the shipping method and destination, with particular attention to moisture protection and coil stability.
A reliable manufacturing process therefore follows a complete chain:
Controlled Chemistry → Casting → Homogenization → Hot Rolling → Cold Rolling → H48 Temper Control → Surface/Coating → Slitting → Inspection → Protective Packaging
This integrated process helps produce 5052 H48 Can End Aluminum Coil with the consistency required for demanding can-end conversion operations.
8. Surface Treatment and Coating of 5052 H48 Coil
Surface treatment and coating help 5052 H48 Can End Aluminum Coil achieve the required corrosion protection, surface quality, and compatibility with the packaged product.
8.1 Surface Cleaning
Before coating, the aluminum surface should be clean and free from oil, dust, grease, oxidation, and other contaminants.
Proper cleaning improves coating adhesion and surface uniformity.
8.2 Surface Pretreatment
When required, a suitable pretreatment can improve:
- Coating adhesion
- Corrosion protection
- Surface stability
- Coating durability
The pretreatment should match the selected coating system and end-use requirements.
8.3 Internal Coating
For can ends, an internal lacquer or protective coating can reduce direct contact between the aluminum and the packaged product.
The coating should provide appropriate resistance to moisture, acids, salts, carbonated contents, and other relevant substances, depending on the application.
8.4 External Coating
External coatings provide additional surface protection and can support printing, decoration, and handling.
The coating must maintain good adhesion and stability during subsequent forming and use.
8.5 Coating Quality Control
Key quality parameters include:
- Coating thickness or weight
- Surface uniformity
- Adhesion
- Curing
- Pinholes
- Chemical resistance
For food and beverage packaging, the coating system should also comply with the applicable food-contact requirements of the target market.
8.6 Bare vs. Coated Coil
| Type | Main Characteristics |
|---|---|
| Bare Coil | Clean aluminum surface for customer-applied coating |
| Pre-Coated Coil | Coated before forming for consistent surface protection |
| Lacquered Coil | Protective or product-contact lacquer for packaging applications |
The choice between bare and coated 5052 H48 coil depends on the production process, coating equipment, can design, and final packaging requirements.
Application of 5052 H48 Can End Aluminum Coil
9. Advantages of 5052 H48 Can End Aluminum Coil
5052 H48 Can End Aluminum Coil provides a combination of material and processing characteristics that can be useful for selected can-end applications.
9.1 Good Corrosion Resistance
5052 belongs to the 5xxx aluminum-magnesium family and provides good resistance to many atmospheric and packaging environments.
When combined with an appropriate coating system, it can provide additional protection against contact with moisture and chemically active contents.
9.2 Higher Strength in H48 Temper
The H48 temper increases the strength and hardness of 5052 through controlled cold working.
This helps the finished can end maintain its shape and resist deformation during handling and use.
9.3 Lightweight Construction
Aluminum has a density of approximately 2.68 g/cm³, making it significantly lighter than many conventional packaging metals.
Using aluminum can help reduce component weight while maintaining the required structural performance.
9.4 Controlled Forming Performance
5052 H48 offers a useful balance between strength and forming capability.
With appropriate thickness, tooling, lubrication, and process control, the coil can support operations such as:
- Blanking
- Shell forming
- Curling
- Scoring
- Riveting
Actual forming performance depends on the complete material and production system.
9.5 Good Surface Quality
A controlled aluminum surface provides a suitable foundation for coating, lacquer, printing, and other finishing processes.
Good surface quality also helps reduce defects during high-speed conversion.
9.6 Consistent Coil Processing
Properly manufactured 5052 H48 coil can provide consistent:
- Thickness
- Width
- Flatness
- Mechanical properties
- Edge condition
- Coil winding
Such consistency is important for automated production lines where material variations can affect production efficiency.
9.7 Coating Compatibility
5052 can be supplied in bare or coated form according to application requirements.
Appropriate coating systems can improve corrosion protection, product compatibility, appearance, and service performance.
9.8 Recyclability
Aluminum is well suited to recycling and can be repeatedly processed into new aluminum products when appropriate collection and recycling systems are available.
This makes aluminum an important material for lightweight packaging solutions.
10. Applications of 5052 H48 Can End Aluminum Coil
5052 H48 Can End Aluminum Coil is used for selected can-end and closure applications where the material requirements call for a balance of strength, corrosion resistance, forming performance, and surface quality.
The final alloy selection should always follow the specific can design and production requirements.
10.1 Beverage Can Ends
5052 H48 can be considered for selected beverage can-end designs where the required strength and forming characteristics match the material specification.
Potential applications include ends for:
- Soft drinks
- Carbonated beverages
- Beer
- Energy drinks
- Other packaged beverages
For pressurized products, engineers should evaluate the complete combination of alloy, temper, thickness, end geometry, scoring design, and internal pressure.
10.2 Food Can Ends
Aluminum can ends can also be used for selected food-packaging applications.
Potential applications include:
- Processed foods
- Canned foods
- Pet food
- Nutritional products
- Specialty food packaging
For these applications, the internal coating is particularly important because the coating separates the aluminum from the packaged product and helps control corrosion.
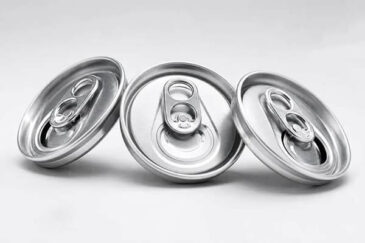
10.3 Easy-Open Can Ends
The material can be processed into selected easy-open closure designs incorporating:
- Opening panels
- Score lines
- Rivets
- Pull tabs
- Stay-on tabs
The score line requires precise control because the finished end must remain secure during storage and handling while allowing controlled opening by the consumer.
10.4 Lightweight Metal Closures
5052 H48 coil can also be considered for lightweight closure and lid components where manufacturers require a combination of:
- Low weight
- Strength
- Corrosion resistance
- Formability
- Surface quality
The exact material specification should correspond to the closure geometry and forming process.
10.5 Specialty Packaging Components
Depending on the customer’s design and technical requirements, 5052 H48 may be considered for customized packaging components and metal closures beyond conventional can ends.
Before mass production, manufacturers should evaluate:
- Material thickness
- Forming behavior
- Score performance
- Coating compatibility
- Sealing performance
- Product-contact requirements
11. 5052 H48 vs. 5182 H48 Aluminum Coil
5052 H48 and 5182 H48 are both 5xxx-series aluminum alloys that can serve demanding packaging and closure applications.
Both provide good corrosion resistance and increased strength through strain hardening, but their alloy chemistry and performance profiles differ.
11.1 Key Differences
| Parameter | 5052 H48 | 5182 H48 |
|---|---|---|
| Alloy Series | 5xxx | 5xxx |
| Main Alloying Element | Magnesium | Magnesium |
| Temper | H48 | H48 |
| Strength Level | High | Generally higher |
| Corrosion Resistance | Good | Good |
| Formability | Good | Good, application-dependent |
| Typical Use | Selected can ends and closures | High-strength can ends and closures |
| Scoring Performance | Requires design-specific control | Requires design-specific control |
| Coating Compatibility | Good | Good |
| Material Selection | Based on can design and forming requirements | Often considered where higher strength is required |
12. Quality Control for 5052 H48 Can End Aluminum Coil
Quality control is essential for 5052 H48 Can End Aluminum Coil because can-end production requires stable mechanical properties, accurate dimensions, and consistent surface quality.
12.1 Chemical Composition Control
The chemical composition is tested to ensure compliance with the specified 5052 alloy requirements. Key elements include Mg, Cr, Fe, Si, Cu, Mn, and Zn.
Consistent chemistry helps maintain stable strength, corrosion resistance, forming performance, and batch-to-batch consistency.
12.2 Dimensional and Mechanical Inspection
Key dimensional checks include:
- Thickness
- Width
- Flatness
- Coil ID and OD
- Coil weight
Mechanical testing typically covers:
- Tensile strength
- Yield strength
- Elongation
- Hardness, when specified
These properties should meet the applicable standard and customer requirements.
12.3 Surface and Edge Quality
The coil surface should remain clean, smooth, and free from major defects such as:
- Scratches
- Dents
- Pits
- Oil stains
- Oxidation
- Surface marks
Edge inspection focuses on cracks, excessive burrs, edge damage, and slitting quality to support stable feeding and blanking.
12.4 Coating Quality
For lacquered or pre-coated coil, quality control may include:
- Coating thickness or weight
- Adhesion
- Curing
- Surface uniformity
- Pinholes
- Chemical resistance
The coating system should match the intended can-end application and applicable food-contact requirements.
12.5 Final Inspection and Traceability
Before shipment, the finished coil undergoes final inspection covering alloy, temper, dimensions, mechanical properties, surface condition, edge quality, coil specifications, and coating condition when applicable.
A Mill Test Certificate (MTC) can provide material and batch information for quality verification and traceability.
13. Conclusion
5052 H48 Can End Aluminum Coil combines the advantages of a 5xxx-series aluminum alloy with the increased strength of the H48 temper.
Its corrosion resistance, lightweight construction, controlled forming performance, and coating compatibility make it suitable for selected can-end and closure applications.
For reliable production, material selection should consider more than alloy and temper.
Thickness, mechanical properties, flatness, surface quality, edge condition, winding quality, scoring requirements, coating system, and can design all influence final performance.
Compared with 5182 H48, 5052 H48 provides a different balance of strength and forming characteristics.
The appropriate alloy should therefore depend on the specific can-end design, production process, performance requirements, and customer specification.
For buyers, a complete purchasing specification should clearly define the 5052 H48 alloy, dimensions, surface condition, coil configuration, applicable standard, mechanical requirements, coating requirements, inspection criteria, and packaging requirements.
With controlled chemistry, precise rolling, stable temper control, careful slitting, and comprehensive inspection, 5052 H48 aluminum coil can provide consistent material performance for demanding packaging production.
FAQs
1. What is 5052 H48 aluminum coil?
5052 H48 is a 5xxx-series aluminum alloy with a strain-hardened H48 temper. It offers good corrosion resistance, increased strength, and controlled forming performance.
2. Can 5052 H48 be used for can ends?
Yes. It can be used for selected can-end and closure applications, depending on the can design, thickness, forming process, and performance requirements.
3. What is the difference between 5052 H48 and 5182 H48?
5182 H48 generally provides higher strength, while 5052 H48 offers a different balance of strength, corrosion resistance, and formability. The final choice depends on the can-end design and production requirements.
4. Can 5052 H48 coil be coated?
Yes. It can be supplied as bare, lacquered, or coated coil, depending on the application and coating requirements.
5. What standards apply to 5052 H48 aluminum coil?
ASTM B209/B209M provides a general specification framework for aluminum sheet and coiled sheet. Specific requirements should follow the applicable customer specification and end use.
6. What quality information should buyers specify?
Buyers should define the alloy, temper, thickness, width, surface, coil dimensions, mechanical requirements, coating, inspection requirements, and MTC to ensure consistent material quality.